How Does Screen Printing Work? One Job Through Our Shop
Lamb Screen Printing ·
Screen printing is simple to describe. Ink gets pushed through a fine mesh screen onto the shirt. The screen is blocked everywhere except where your design is, so the ink only goes through there. Every color in the design gets its own screen, and the colors go down one after another. Then heat cures the ink so it holds up in the wash.
You’ll still hear it called silk screening. The screens haven’t been silk for a long time.
What changes from shop to shop is how the screens get made and what happens around the press. Here’s how a job actually goes through our shop in San Marcos, who does each part, and what it means for your order.
How a job goes through our shop
- I separate your art into one layer for each ink color. Most jobs are spot color, and I do those by hand. Full-color designs go through separation software.
- The screens get coated with a light-sensitive emulsion on a coating machine.
- Juan images each screen on our laser imager, one screen per color, straight from the file.
- Juan hangs the screens on our automatic press, lines them up and prints. On a dark shirt, a white underbase goes down first, and a flash dryer sets it before the colors go on top.
- The shirts ride through our dryer to cure.
- Gavin or my dad Rex catches them coming off the dryer, and they get folded and bagged.
- They’re boxed for pickup or shipping.
- The screens get stripped and cleaned for the next job.
Alison handles most of the quoting and email, and orders the blank garments. I do some of that too. Gavin and Juan also press the DTF transfers we use for names, numbers and small runs. My mom, Kathy, keeps the books. The customer side of all this, from quote to pickup, is on our what to expect page.
No film
The traditional way to make a screen, and still how a lot of shops do it, is to print the design onto clear film, lay it on the coated screen and expose it to light. We don’t use film. Our laser writes the design straight onto the coated screen.
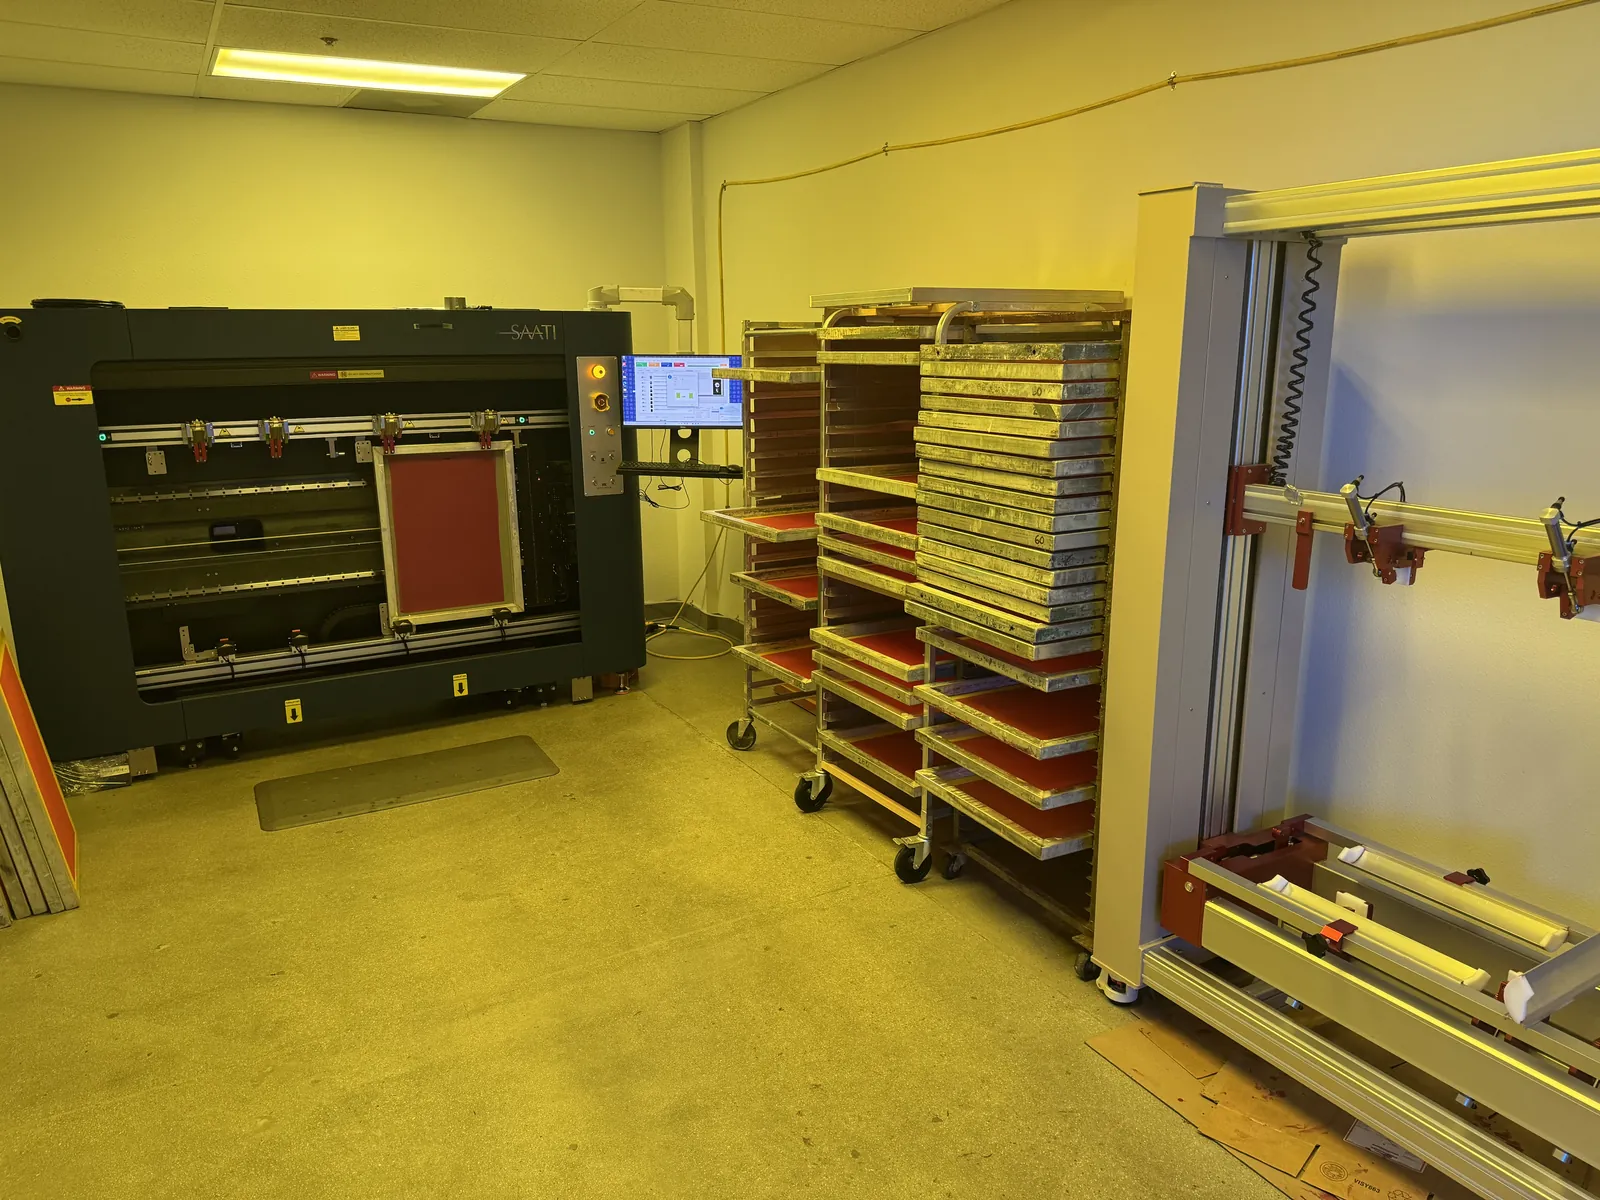
What you’d notice is sharper detail, and reorders that come out more precise. It’s faster for us too. We make fresh screens for every job, reorders included.
Spot color, and the other kinds
At least half of our jobs are spot color. Each color in the design is its own solid ink, the way most logos are printed.
We also run the other kinds: simulated process, halftones and grayscale. They build shading, gradients and photo-like images out of tiny dots in a handful of inks, which is how a detailed design gets printed without a separate ink for every shade.
Every color is another screen and another setup, which is why the number of colors moves the price. Our automatic press prints up to eight colors, and a design with a lot of colors gets very tricky on it.
The white underbase
On a dark shirt, we print a white layer first so the colors stay bright, set it with the flash dryer, and put the colors on top of it. That’s the underbase. We don’t charge for it as an extra color.
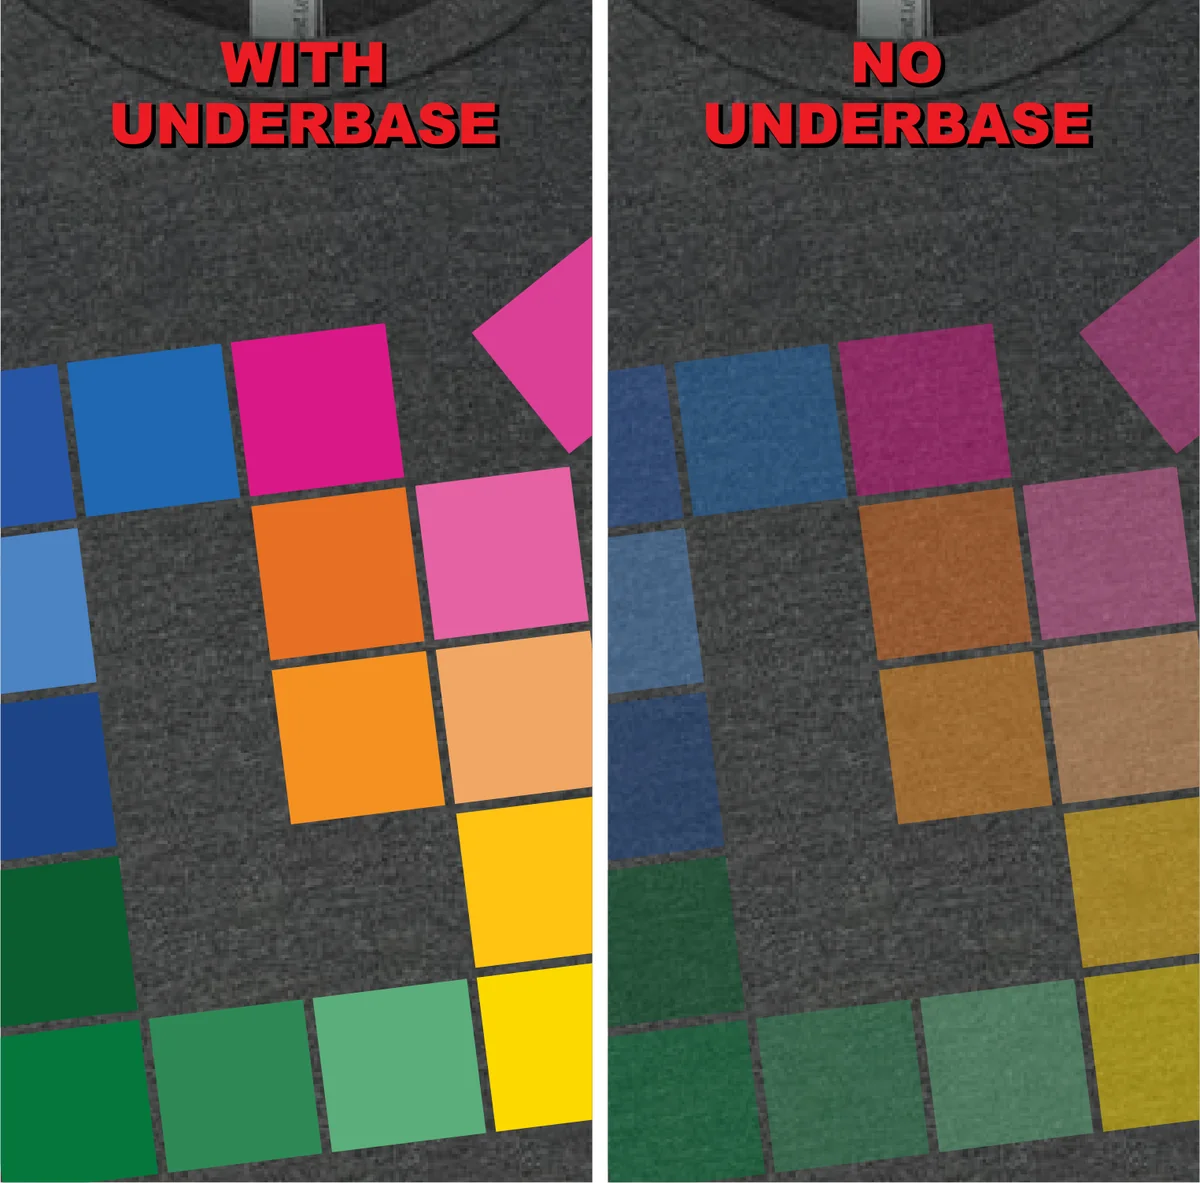
Some customers skip it on purpose. Without an underbase the print feels softer and looks more vintage. It’s a case-by-case call, and it’s yours to make.
Most of what we print is plastisol ink. For water-based discharge, specialty inks like puff and metallic, and what polyester does to ink, see our DTF vs screen printing page.
Curing
A print isn’t finished when it comes off the press. The ink has to be cured with heat so it lasts. Every shirt rides through our 20-foot gas tunnel dryer, somewhere between the low 200s and the mid 300s Fahrenheit, depending on the job. We check the cure two ways: a temperature gun, and a stretch test, where we pull the print to make sure it doesn’t crack.
What screen printing is bad at
First-time buyers are usually surprised by size and placement.
Our standard maximum print is 14 by 15 inches. If your design needs to be bigger, ask before you plan on it.
We’ll print over a seam on some jobs, not all.
All-over printing, edge to edge across the whole shirt, usually takes a belt printer. We don’t have one, so we don’t do it.
And if you only need a handful of pieces, especially with a lot of colors, DTF is often the better call. That’s all on our DTF vs screen printing page.
Getting a quote
If you have a design and a rough count, send it through our quote form: the garments and roughly how many of each, the date you need them in hand, and the art, even if it’s only a sketch or a logo file. Tell us if the garments are dark, if the print is big, or if the design has a lot of colors, and we’ll tell you how we’d print it. If the shirts are your own, read how we handle customer-supplied garments first.